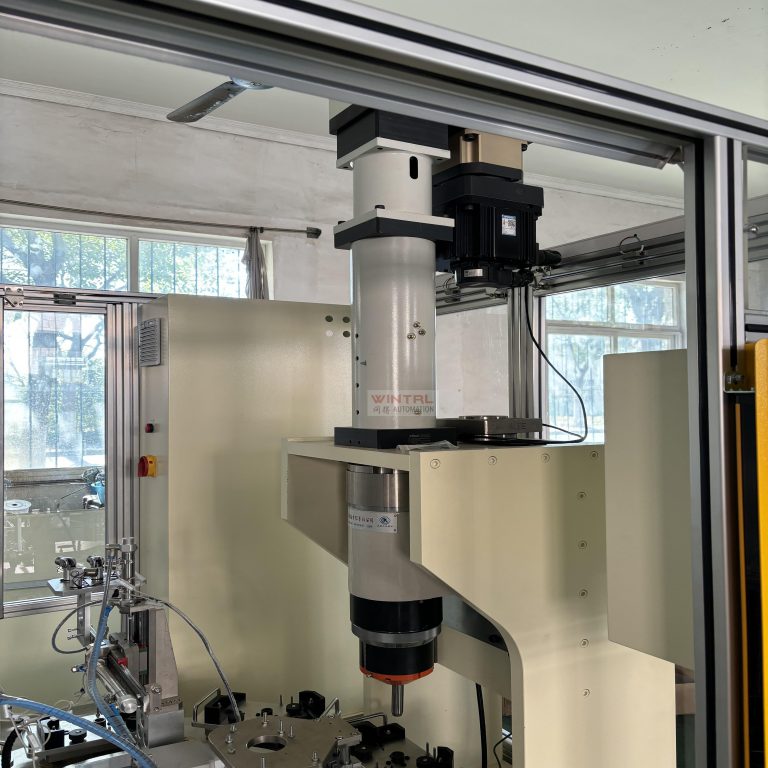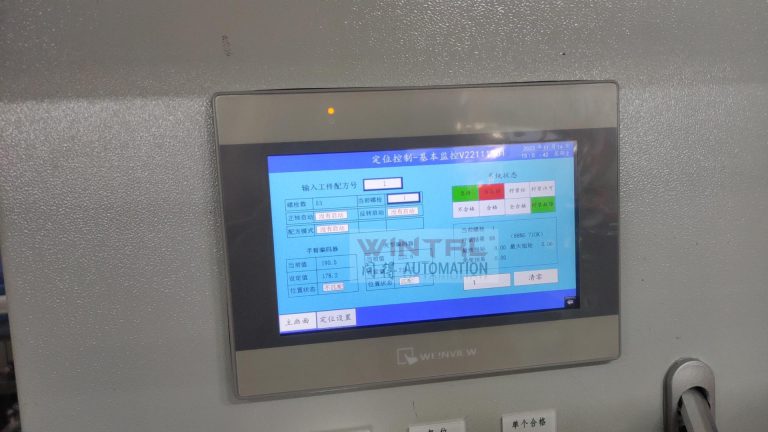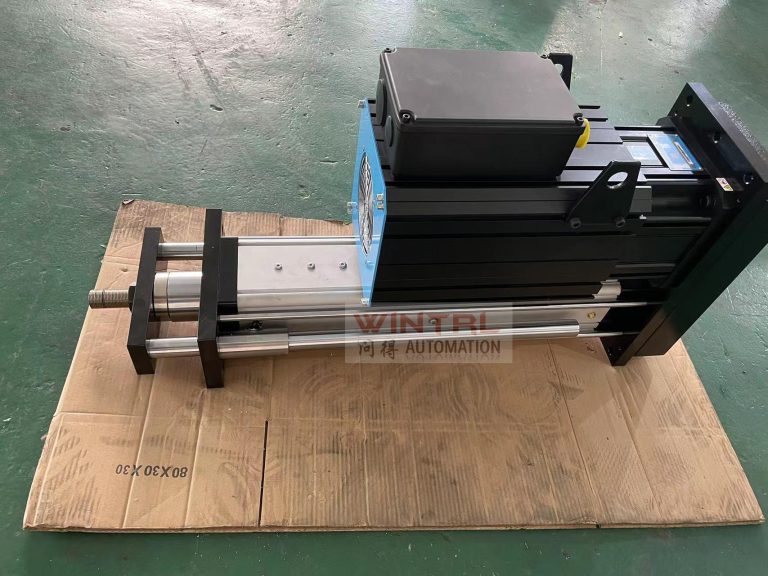
Key Conclusions:The standard cycle for a servo press is as follows: workpiece positioning and verification, rapid advance, contact detection, press-fitting phase, pressure holding, return stroke, curve evaluation, and data archiving. The key to operation lies not in the sequence of button presses, but in the optimal combination of speeds, target positions, and target pressures for each phase.
Core Components and Control Logic
Use a higher speed during the rapid-feed section to shorten the cycle time, but switch to low speed when within 5–10 mm of the workpiece to avoid impact damage to the workpiece or the ram.
Detect the contact point using a pressure surge as the trigger condition, then switch to force control or a combination of position and force control; this step determines whether the starting points of the curves are consistent.
Details That Are Easily Overlooked During Implementation
- The WL-FT-V1 dedicated controller supports storing multiple sets of recipes; when switching between production runs, you can simply call up the recipe instead of having to reset each parameter individually.
- The pressure-holding stage is used for processes—such as those involving bushings and seals—that require stress relief; the duration is generally determined through process testing, as an excessively long duration will only slow down the production cycle.
- At the end of each cycle, the system should automatically indicate "OK" or "NG." "NG" items should be prevented from proceeding to the next station via an interlock mechanism, rather than relying solely on an alarm.
Verification of Key Parameters for Servo Presses
| Project | Key Metrics / Configuration |
|---|---|
| Repeatability | ±0.02 mm |
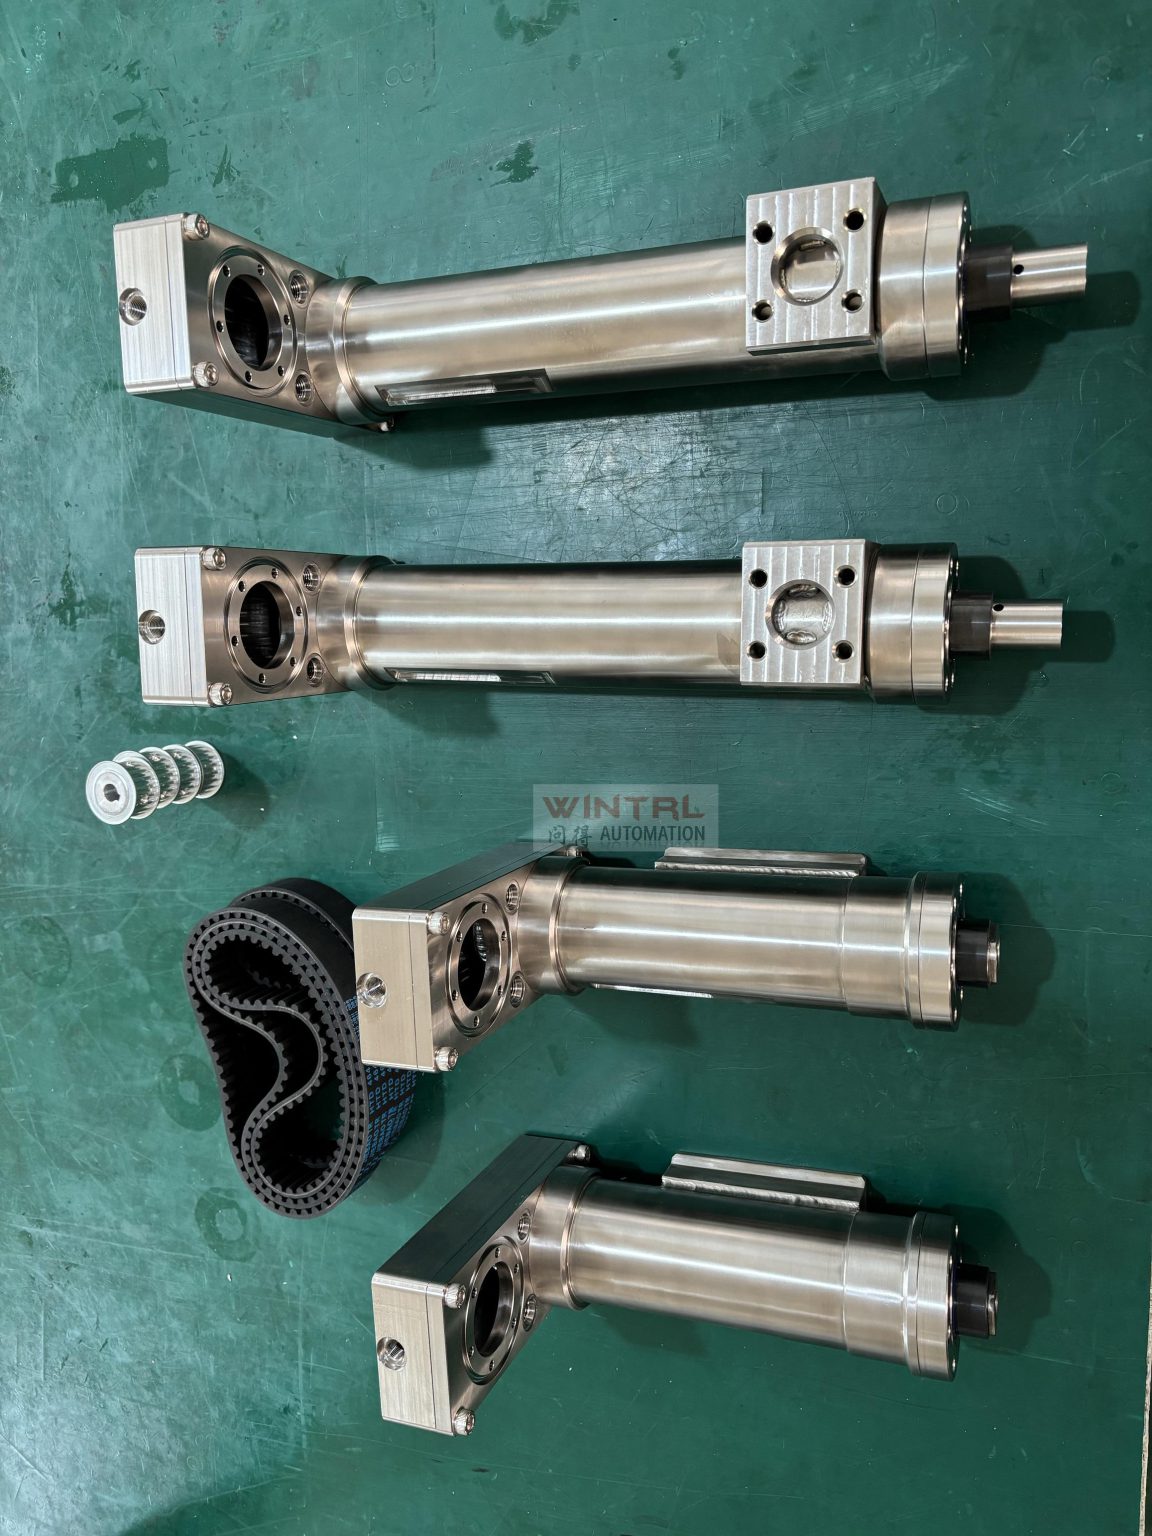
| Pressure Sensor | 1,000 kg (74 mm) or 2,000 kg (104 mm), with an accuracy of approximately one-thousandth of the full scale |
| Motor Power | 0.75 / 1.0 / 1.5 / 2.5 kW |
| Power Supply | 220 V AC (1.5 kW, 380 V optional) |
| Controller | WL-FT-V1 Dedicated Controller, or PLC + Touchscreen / PC Software |
| Software and Data | Curve display, 16 parameter presets, CSV export, PC interface |
Related Equipment and Further Reading
When implementing the project, you can directly refer to WINTRL’s existing equipment selection:Servo Press Motor Rotor Press-Fit Machine、High-Speed Chain Automated Assembly Line、Engine Rocker Arm Assembly Line。
For systematic principles and selection methods, see The Complete Guide to Servo Presses; For a complete list of models and specifications, see Product Center。
Frequently Asked Questions
Do I have to re-calibrate every time I switch products?
Save proven processes as recipes and assign them numbers; when switching between product types, simply call up the appropriate recipe—only the first-piece inspection is required.
Is a faster press-fitting speed always better?
No. You must slow down as you approach the contact point; otherwise, the impact will damage both the workpiece and the pressure sensor.
If you need to calculate thrust, stroke, or the determination window based on your workpiece, or if you would like to request technical documentation, please visitDownload Product Brochures、prescription, or directly through Contact Us Submit your operating conditions, and engineers from Shanghai WINTRL Automation will provide product selection recommendations. For company background, seeAbout Us。